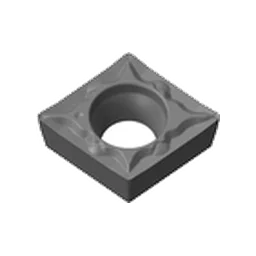
CCMT 09T308 车削刀片
对比 合适的材料与应用, ,然后选择 a brand 查看 the exact SKUs.
- ISO Code
- CCMT09T308
- 刀片尺寸
- 09T308
- Shape
- C
查找合适的选项
Select the workpiece material and application. 品牌 remains optional.
Brands
该父型号的全部可选规格。
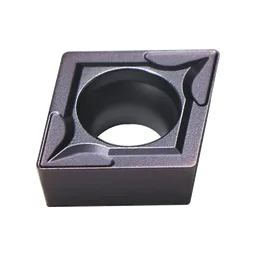
CCMT 09T308 is an 80° rhombic turning insert with 4 usable cutting edges, used mainly for general turning and profiling. We list 52 stock-keeping variants of it from Achteck, HADSTO, covering 钢, 不锈钢, 铸铁, 有色金属.
The designation encodes the geometry: the first letter is the shape (C), the following letter the clearance angle, then the tolerance class, then size, thickness and nose radius. If you want to check any of it, our ISO insert code decoder breaks the full string down character by character.
Geometry and dimensions
| Insert family | CCMT |
|---|---|
| Category | 车削刀片 |
| Shape | 80° rhombic (C) |
| Usable cutting edges | 4 |
| 内切圆直径 (IC) | 9.53 mm |
| 厚度 (S) | 3.97 mm |
| 刀尖圆角 (RE) | 0.8 mm |
| Fixing hole diameter (D1) | 4.4 mm |
| Hand | Neutral |
| Variants in stock | 52 |
| Brands | Achteck, HADSTO |
Recommended cutting data
The figures below are the manufacturers' published ranges, aggregated across the 52 variants listed on this page. The typical column is the median, which is where most shops end up running. Treat the full range as the envelope, not a target — start around 60–70% of it and work up.
| 工件材料 | Cutting speed vc (m/min) | Typical vc | Feed fn (mm/rev) | Depth of cut ap (mm) | Variants with data |
|---|---|---|---|---|---|
| 钢 (P) | 45 – 620 | 50 – 200 | 0.04–0.36 | 0.06–3.5 | 28 of 52 |
| 不锈钢 (M) | 70 – 250 | 85 – 200 | 0.09–0.36 | 0.3–3.5 | 15 of 52 |
| 铸铁 (K) | 50 – 490 | 50 – 200 | 0.04–0.36 | 0.1–3.5 | 10 of 52 |
| 耐热合金 (S) | 20 – 200 | 30 – 90 | 0.09–0.36 | 0.6–3.2 | 14 of 52 |
To turn a cutting speed into a spindle speed for your actual diameter, use the cutting parameters calculator: n = vc × 1000 / (π × D).
Carbide grades available
52 variants of CCMT 09T308 are stocked in these grades: AT202, AT210A, AP200U, AC052P, AC152P, AC100M, AC200M, AC252P, AP301M, AP200M, HS6120, HS7125, HS7225, HS8115 and others.
Across this range the grades specified most often are AT202, AT210A, AP200U, AC052P, AC152P. Within one brand's range, a higher middle digit usually means a tougher grade — better on interrupted cuts, slightly less wear resistant. See carbide grades explained for how to read the names.
槽型 geometries
断屑槽 stocked for CCMT 09T308: KC2, PC2, PB1, PA1, F1T, F2K, M2T, PB2.
The chipbreaker sets the usable feed window far more than the depth of cut does. A roughing geometry run at finishing feed will not break the chip; a finishing geometry pushed into a roughing cut will chip. Match it to the feed you will actually run — chipbreaker selection guide.
Typical applications
- 精加工
- 中加工
- 粗加工
For more on cutting steel, see our material-specific guide.
Choosing the right CCMT 09T308
Three things decide which variant you need:
- The workpiece material group. This page lists variants published for 钢, 不锈钢, 铸铁, 有色金属, 耐热合金. Pick a grade from the group you are cutting — a steel grade on a superalloy will fail quickly.
- Feed, not depth of cut. The chipbreaker is defined by its feed window. Decide the feed first, then pick the geometry that covers it.
- 刀尖圆角 versus finish. CCMT 09T308 is stocked here at 0.8 mm. A larger radius gives better finish at the same feed and a stronger edge, but raises cutting force.
Not sure whether CCMT 09T308 is the right shape at all? The turning insert selection guide compares shapes by what the part profile allows.
Frequently asked questions about CCMT 09T308
What size insert is CCMT 09T308?
CCMT 09T308 has an inscribed circle of 9.53 mm and a thickness of 3.97 mm. As a rule the depth of cut should stay under about two thirds of the inscribed circle.
What nose radius does CCMT 09T308 have?
The nose radius (the last two digits of the designation) is 0.8 mm on the variants listed here. Surface roughness scales roughly with fn²/(32 × RE), so at a fixed feed a larger radius halves Ra.
Which holder does CCMT 09T308 fit?
The holder designation must carry the same shape letter (C) and the same size digit. Send us your holder code and we will confirm the match before you order.
How many CCMT 09T308 variants do you stock?
52 variants from Achteck, HADSTO, listed below with grade, chipbreaker and the published cutting data where the manufacturer provides it.
What cutting speed should I run for CCMT 09T308?
For 钢, the published range across these variants is 45–620 m/min, with a typical window of 50–200 m/min. Heavy cuts sit at the bottom of that range, light finishing cuts at the top.
Related
- Same family: CCMT 09T304, CCMT 060204, CCMT 060208, CCMT 120408, CCMT 120404, CCMT 060202, CCMT 120412, CCMT 09T302
- All CCMT
- HADSTO CCMT 09T308 (5 variants)
- Achteck CCMT 09T308 (47 variants)
- Decode the CCMT 09T308 designation
- Cutting speed to rpm calculator
- Turning insert selection guide