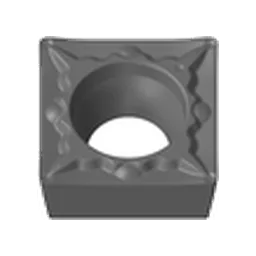
SCMT 09T304 Turning Inserts
Compare suitable materials and applications, then choose a brand to view the exact SKUs.
- ISO Code
- SCMT09T304
- Insert Size
- 09T304
- Shape
- S
Find the Right Option
Select the workpiece material and application. Brand remains optional.
Brands
All available options for this parent model.
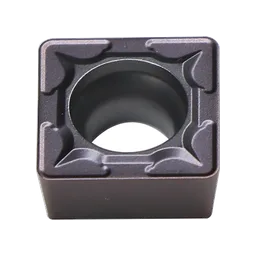
This page covers every SCMT 09T304 insert we can supply — 41 variants across Achteck, HADSTO, published for Steel, Stainless steel, Cast iron, Non-ferrous. The square 90° geometry gives it 8 cutting edges and makes it suitable for heavy roughing, square shoulders and interrupted cuts.
The designation encodes the geometry: the first letter is the shape (S), the following letter the clearance angle, then the tolerance class, then size, thickness and nose radius. If you want to check any of it, our ISO insert code decoder breaks the full string down character by character.
Geometry and dimensions
| Insert family | SCMT |
|---|---|
| Category | Turning Inserts |
| Shape | square 90° (S) |
| Usable cutting edges | 8 |
| Inscribed circle (IC) | 9.53 mm |
| Thickness (S) | 3.97 mm |
| Nose radius (RE) | 0.4 mm |
| Fixing hole diameter (D1) | 4.4 mm |
| Hand | Neutral |
| Variants in stock | 41 |
| Brands | Achteck, HADSTO |
Recommended cutting data
The figures below are the manufacturers' published ranges, aggregated across the 41 variants listed on this page. The typical column is the median, which is where most shops end up running. Treat the full range as the envelope, not a target — start around 60–70% of it and work up.
| Workpiece material | Cutting speed vc (m/min) | Typical vc | Feed fn (mm/rev) | Depth of cut ap (mm) | Variants with data |
|---|---|---|---|---|---|
| Steel (P) | 45 – 620 | 75 – 250 | 0.04–0.3 | 0.3–3.5 | 19 of 41 |
| Stainless steel (M) | 70 – 250 | 85 – 200 | 0.04–0.3 | 0.3–3.14 | 13 of 41 |
| Cast iron (K) | 50 – 490 | 50 – 200 | 0.04–0.25 | 0.3–3.5 | 7 of 41 |
| Heat-resistant alloys (S) | 20 – 200 | 30 – 85 | 0.04–0.18 | 0.3–3.1 | 12 of 41 |
To turn a cutting speed into a spindle speed for your actual diameter, use the cutting parameters calculator: n = vc × 1000 / (π × D).
Carbide grades available
41 variants of SCMT 09T304 are stocked in these grades: AP200U, AT202, AT210A, AC052P, AC100M, AC152P, AC200M, AC252P, AP200M, AP301M, HS6120, HS7125, HS7225, HS8115 and others.
Across this range the grades specified most often are AP200U, AT202, AT210A, AC052P, AC100M. Within one brand's range, a higher middle digit usually means a tougher grade — better on interrupted cuts, slightly less wear resistant. See carbide grades explained for how to read the names.
Chipbreaker geometries
Chipbreakers stocked for SCMT 09T304: KC2, PC2, PB1, M2T, PB2.
The chipbreaker sets the usable feed window far more than the depth of cut does. A roughing geometry run at finishing feed will not break the chip; a finishing geometry pushed into a roughing cut will chip. Match it to the feed you will actually run — chipbreaker selection guide.
Typical applications
- Medium
- Roughing
- Finishing
For more on cutting steel, see our material-specific guide.
Choosing the right SCMT 09T304
Three things decide which variant you need:
- The workpiece material group. This page lists variants published for Steel, Stainless steel, Cast iron, Non-ferrous, Heat-resistant alloys. Pick a grade from the group you are cutting — a steel grade on a superalloy will fail quickly.
- Feed, not depth of cut. The chipbreaker is defined by its feed window. Decide the feed first, then pick the geometry that covers it.
- Nose radius versus finish. SCMT 09T304 is stocked here at 0.4 mm. A larger radius gives better finish at the same feed and a stronger edge, but raises cutting force.
Not sure whether SCMT 09T304 is the right shape at all? The turning insert selection guide compares shapes by what the part profile allows.
Frequently asked questions about SCMT 09T304
What size insert is SCMT 09T304?
SCMT 09T304 has an inscribed circle of 9.53 mm and a thickness of 3.97 mm. As a rule the depth of cut should stay under about two thirds of the inscribed circle.
What nose radius does SCMT 09T304 have?
The nose radius (the last two digits of the designation) is 0.4 mm on the variants listed here. Surface roughness scales roughly with fn²/(32 × RE), so at a fixed feed a larger radius halves Ra.
Which holder does SCMT 09T304 fit?
The holder designation must carry the same shape letter (S) and the same size digit. Send us your holder code and we will confirm the match before you order.
How many SCMT 09T304 variants do you stock?
41 variants from Achteck, HADSTO, listed below with grade, chipbreaker and the published cutting data where the manufacturer provides it.
What cutting speed should I run for SCMT 09T304?
For Steel, the published range across these variants is 45–620 m/min, with a typical window of 75–250 m/min. Heavy cuts sit at the bottom of that range, light finishing cuts at the top.
Related
- Same family: SCMT 09T308, SCMT 120404, SCMT 120408, SCMT 120412, SCMT 380932
- All SCMT
- HADSTO SCMT 09T304 (5 variants)
- Achteck SCMT 09T304 (36 variants)
- Decode the SCMT 09T304 designation
- Cutting speed to rpm calculator
- Turning insert selection guide