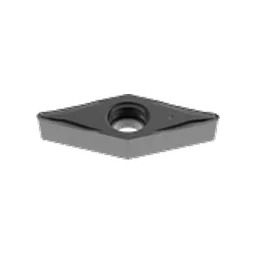
Achteck VBMT
Achteck VBMT 160408 Turning Inserts
BrandAchteckISO ModelVBMT160408Available MaterialsPMSKAvailable Options53
Available Applications
FinishingMediumRoughing
Specification
- ISO Code
- VBMT160408
- Insert Size
- 160408
- Shape
- V
- Radius
- 0.8 mm
- Thickness
- 4.76 mm
- D / IC
- 9.52 mm
- Hole Diameter
- 4.4 mm
- Available Materials
- PMSK
- Available Applications
- Finishing, Medium, Roughing
Product Overview
Achteck VBMT160408 inserts are grouped by the shared ISO parent model. Grade, chipbreaker, material suitability and technical parameters remain attached to each exact SKU.
Filter the table below and add the exact model you need to the RFQ basket.
Achteck VBMT160408
53 Available Options
| Full Model | Material | Application | Grade | Chipbreaker | Product No. | Quantity | Action |
|---|---|---|---|---|---|---|---|
VBMT 160408E-PB2 AP200U | PM | Finishing, Medium | AP200U | PB2 | 80088141 | ||
VBMT 160408E-PB2 AP010S | MS | Finishing, Medium | AP010S | PB2 | 80107028 | ||
VBMT 160408E-PA1 AC052P | P | Finishing | AC052P | PA1 | 80055148 | ||
VBMT 160408E-PA1 AC152P | P | Finishing | AC152P | PA1 | 80055412 | ||
VBMT 160408E-PB1 AC202P | P | Finishing | AC202P | PB1 | 80143105 | ||
VBMT 160408E-PC2 AC202P | P | Medium | AC202P | PC2 | 80143093 | ||
VBMT 160408E-BS AC052P | P | Finishing | AC052P | BS | 80060686 | ||
VBMT 160408E-BS AC152P | P | Finishing | AC152P | BS | 80060700 | ||
VBMT 160408E-BS AC252P | P | Finishing | AC252P | BS | 80060714 | ||
VBMT 160408E-BS AT202 | PK | Finishing | AT202 | BS | 80048512 | ||
VBMT 160408E-BS AT210A | P | Finishing | AT210A | BS | 80048455 | ||
VBMT 160408E-KC2 AC052P | P | Roughing | AC052P | KC2 | 80051399 | ||
VBMT 160408E-KC2 AC100K | K | Roughing | AC100K | KC2 | 00002175 | ||
VBMT 160408E-KC2 AC100M | MS | Roughing | AC100M | KC2 | 80044297 | ||
VBMT 160408E-KC2 AC102K | K | Roughing | AC102K | KC2 | 80043457 | ||
VBMT 160408E-KC2 AC152P | P | Roughing | AC152P | KC2 | 80052447 | ||
VBMT 160408E-KC2 AC200M | MS | Roughing | AC200M | KC2 | 80044116 | ||
VBMT 160408E-KC2 AC202K | K | Roughing | AC202K | KC2 | 80043303 | ||
VBMT 160408E-KC2 AC252P | P | Roughing | AC252P | KC2 | 80052801 | ||
VBMT 160408E-KC2 AC350P | P | Roughing | AC350P | KC2 | 00034860 | ||
VBMT 160408E-KC2 AP200M | M | Roughing | AP200M | KC2 | 80040477 | ||
VBMT 160408E-KC2 AP200U | MS | Roughing | AP200U | KC2 | 80048967 | ||
VBMT 160408E-KC2 AT202 | PK | Roughing | AT202 | KC2 | 80028638 | ||
VBMT 160408E-KC2 AT210A | P | Roughing | AT210A | KC2 | 80059770 | ||
VBMT 160408E-KC2(O) AC052P | P | Roughing | AC052P | KC2 | 80051400 | ||
VBMT 160408E-KC2(O) AC152P | P | Roughing | AC152P | KC2 | 80052448 | ||
VBMT 160408E-KC2(O) AC252P | P | Roughing | AC252P | KC2 | 80052802 | ||
VBMT 160408E-PA1 AT202 | PK | Finishing | AT202 | PA1 | 80055977 | ||
VBMT 160408E-PA1 AT210A | P | Finishing | AT210A | PA1 | 80060505 | ||
VBMT 160408E-PB1 AC052P | P | Finishing | AC052P | PB1 | 80051386 | ||
VBMT 160408E-PB1 AC100M | MS | Finishing | AC100M | PB1 | 80044232 | ||
VBMT 160408E-PB1 AC152P | P | Finishing | AC152P | PB1 | 80052434 | ||
VBMT 160408E-PB1 AC200M | MS | Finishing | AC200M | PB1 | 80044050 | ||
VBMT 160408E-PB1 AC252P | P | Finishing | AC252P | PB1 | 80052788 | ||
VBMT 160408E-PB1 AP200M | PM | Finishing | AP200M | PB1 | 80028706 | ||
VBMT 160408E-PB1 AP200U | MS | Finishing | AP200U | PB1 | 80048901 | ||
VBMT 160408E-PB1 AP301M | MS | Finishing | AP301M | PB1 | 00025268 | ||
VBMT 160408E-PB1 AT202 | PK | Finishing | AT202 | PB1 | 80028632 | ||
VBMT 160408E-PB1 AT210A | P | Finishing | AT210A | PB1 | 80059764 | ||
VBMT 160408E-PC2 AC052P | P | Medium | AC052P | PC2 | 80051392 | ||
VBMT 160408E-PC2 AC100M | MS | Medium | AC100M | PC2 | 80044266 | ||
VBMT 160408E-PC2 AC152P | P | Medium | AC152P | PC2 | 80052440 | ||
VBMT 160408E-PC2 AC200M | MS | Medium | AC200M | PC2 | 80044085 | ||
VBMT 160408E-PC2 AC252P | P | Medium | AC252P | PC2 | 80052794 | ||
VBMT 160408E-PC2 AP010S | MS | Medium | AP010S | PC2 | 80056062 | ||
VBMT 160408E-PC2 AP100S | MS | Medium | AP100S | PC2 | 00035079 | ||
VBMT 160408E-PC2 AP200M | PM | Medium | AP200M | PC2 | 80028705 | ||
VBMT 160408E-PC2 AP200U | MS | Medium | AP200U | PC2 | 80048936 | ||
VBMT 160408E-PC2 AP301M | MS | Medium | AP301M | PC2 | 00024485 | ||
VBMT 160408E-PC2 AT202 | PK | Medium | AT202 | PC2 | 80028636 | ||
VBMT 160408E-PC2 AT210A | P | Medium | AT210A | PC2 | 80059768 | ||
VBMT 160408-F2K AT202 | PK | Finishing | AT202 | F2K | 80084636 | ||
VBMT 160408-F2K AT210A | P | Finishing | AT210A | F2K | 80101459 |
Cutting data and geometry (53 SKUs)
VBMT 160408E-PB2 AP200U
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.8-3.5
Feed (f)0.10-0.40
Cutting speed P100-200
Cutting speed M70-200
DirectionNeutral
Weight8.4
VBMT 160408E-PB2 AP010S
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.8-3.5
Feed (f)0.10-0.40
Cutting speed M100-250
Cutting speed S30-120
DirectionNeutral
Weight8.5
VBMT 160408E-PA1 AC052P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.10-1.00
Feed (f)0.05-0.30
Cutting speed P105-620
DirectionNeutral
Weight0.0083
VBMT 160408E-PA1 AC152P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.10-1.00
Feed (f)0.05-0.30
Cutting speed P95-570
DirectionNeutral
Weight0.0082
VBMT 160408E-PB1 AC202P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.60-2.1
Feed (f)0.09-0.28
Cutting speed P150-400
DirectionNeutral
Weight0.0086
VBMT 160408E-PC2 AC202P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.70-3.1
Feed (f)0.10-0.32
Cutting speed P150-400
DirectionNeutral
Weight0.0082
VBMT 160408E-BS AC052P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-1.50
Feed (f)0.05-0.20
Cutting speed P105-620
DirectionNeutral
Weight0.0084
VBMT 160408E-BS AC152P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-1.50
Feed (f)0.05-0.20
Cutting speed P95-570
DirectionNeutral
Weight0.0083
VBMT 160408E-BS AC252P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-1.50
Feed (f)0.05-0.20
Cutting speed P75-510
DirectionNeutral
Weight0.0082
VBMT 160408E-BS AT202
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-1.50
Feed (f)0.05-0.20
Cutting speed P50-200
Cutting speed K50-200
DirectionNeutral
Weight0.0041
VBMT 160408E-BS AT210A
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-1.50
Feed (f)0.05-0.20
Cutting speed P50-180
DirectionNeutral
Weight0.0041
VBMT 160408E-KC2 AC052P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-3.3
Feed (f)0.12-0.36
Cutting speed P105-620
DirectionNeutral
Weight0.0082
VBMT 160408E-KC2 AC100K
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.8-3.32
Feed (f)0.12-0.36
Cutting speed K125-490
DirectionNeutral
WeightNULL
VBMT 160408E-KC2 AC100M
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-3.3
Feed (f)0.12-0.36
Cutting speed M130-250
Cutting speed S30-80
DirectionNeutral
Weight0.0082
VBMT 160408E-KC2 AC102K
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-3.3
Feed (f)0.12-0.36
Cutting speed K125-490
DirectionNeutral
Weight0.0087
VBMT 160408E-KC2 AC152P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-3.3
Feed (f)0.12-0.36
Cutting speed P95-570
DirectionNeutral
Weight0.0081
VBMT 160408E-KC2 AC200M
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-3.3
Feed (f)0.12-0.36
Cutting speed M100-200
Cutting speed S20-70
DirectionNeutral
Weight0.0085
VBMT 160408E-KC2 AC202K
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-3.3
Feed (f)0.12-0.36
Cutting speed K95-400
DirectionNeutral
Weight0.0087
VBMT 160408E-KC2 AC252P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-3.3
Feed (f)0.12-0.36
Cutting speed P75-510
DirectionNeutral
Weight0.008
VBMT 160408E-KC2 AC350P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-3.3
Feed (f)0.12-0.36
Cutting speed P45-250
DirectionNeutral
Weight0.008
VBMT 160408E-KC2 AP200M
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.8-3.32
Feed (f)0.12-0.36
DirectionNeutral
Weight0.0084
VBMT 160408E-KC2 AP200U
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-3.3
Feed (f)0.12-0.36
Cutting speed M70-200
Cutting speed S30-90
DirectionNeutral
Weight0.0084
VBMT 160408E-KC2 AT202
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-3.3
Feed (f)0.12-0.36
Cutting speed P50-200
Cutting speed K50-200
DirectionNeutral
Weight0.0039
VBMT 160408E-KC2 AT210A
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-3.3
Feed (f)0.12-0.36
Cutting speed P50-180
DirectionNeutral
Weight0.004
VBMT 160408E-KC2(O) AC052P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-3.3
Feed (f)0.12-0.36
Cutting speed P105-620
DirectionNeutral
Weight0.0083
VBMT 160408E-KC2(O) AC152P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-3.3
Feed (f)0.12-0.36
Cutting speed P95-570
DirectionNeutral
Weight0.0082
VBMT 160408E-KC2(O) AC252P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.80-3.3
Feed (f)0.12-0.36
Cutting speed P75-510
DirectionNeutral
Weight0.0081
VBMT 160408E-PA1 AT202
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.10-1.00
Feed (f)0.05-0.30
Cutting speed P50-200
Cutting speed K50-200
DirectionNeutral
Weight0.004
VBMT 160408E-PA1 AT210A
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.10-1.00
Feed (f)0.05-0.30
Cutting speed P50-180
DirectionNeutral
Weight0.0041
VBMT 160408E-PB1 AC052P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.60-2.1
Feed (f)0.09-0.28
Cutting speed P105-620
DirectionNeutral
Weight0.0087
VBMT 160408E-PB1 AC100M
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.60-2.1
Feed (f)0.09-0.28
Cutting speed M130-250
Cutting speed S30-80
DirectionNeutral
Weight0.0087
VBMT 160408E-PB1 AC152P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.60-2.1
Feed (f)0.09-0.28
Cutting speed P95-570
DirectionNeutral
Weight0.0086
VBMT 160408E-PB1 AC200M
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.60-2.1
Feed (f)0.09-0.28
Cutting speed M100-200
Cutting speed S20-70
DirectionNeutral
Weight0.009
VBMT 160408E-PB1 AC252P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.60-2.1
Feed (f)0.09-0.28
Cutting speed P75-510
DirectionNeutral
Weight0.0085
VBMT 160408E-PB1 AP200M
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.6-2.08
Feed (f)0.09-0.28
DirectionNeutral
Weight0.0089
VBMT 160408E-PB1 AP200U
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.60-2.1
Feed (f)0.09-0.28
Cutting speed M70-200
Cutting speed S30-90
DirectionNeutral
Weight0.0089
VBMT 160408E-PB1 AP301M
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.60-2.1
Feed (f)0.09-0.28
Cutting speed M70-200
Cutting speed S30-160
DirectionNeutral
Weight0.00891
VBMT 160408E-PB1 AT202
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.60-2.1
Feed (f)0.09-0.28
Cutting speed P50-200
Cutting speed K50-200
DirectionNeutral
Weight0.0042
VBMT 160408E-PB1 AT210A
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.60-2.1
Feed (f)0.09-0.28
Cutting speed P50-180
DirectionNeutral
Weight0.0043
VBMT 160408E-PC2 AC052P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.70-3.1
Feed (f)0.10-0.32
Cutting speed P105-620
DirectionNeutral
Weight0.0082
VBMT 160408E-PC2 AC100M
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.70-3.1
Feed (f)0.10-0.32
Cutting speed M130-250
Cutting speed S30-80
DirectionNeutral
Weight0.0083
VBMT 160408E-PC2 AC152P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.70-3.1
Feed (f)0.10-0.32
Cutting speed P95-570
DirectionNeutral
Weight0.0081
VBMT 160408E-PC2 AC200M
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.70-3.1
Feed (f)0.10-0.32
Cutting speed M100-200
Cutting speed S20-70
DirectionNeutral
Weight0.0086
VBMT 160408E-PC2 AC252P
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.70-3.1
Feed (f)0.10-0.32
Cutting speed P75-510
DirectionNeutral
Weight0.008
VBMT 160408E-PC2 AP010S
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.70-3.1
Feed (f)0.10-0.32
Cutting speed M100-250
Cutting speed S30-120
DirectionNeutral
Weight0.0085
VBMT 160408E-PC2 AP100S
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.7-3.11
Feed (f)0.1-0.32
Cutting speed M85-240
Cutting speed S30-200
DirectionNeutral
Weight0.0087
VBMT 160408E-PC2 AP200M
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.70-3.1
Feed (f)0.10-0.32
DirectionNeutral
Weight0.0084
VBMT 160408E-PC2 AP200U
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.70-3.1
Feed (f)0.10-0.32
Cutting speed M70-200
Cutting speed S30-90
DirectionNeutral
Weight0.0084
VBMT 160408E-PC2 AP301M
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.7-3.11
Feed (f)0.1-0.32
Cutting speed M70-200
Cutting speed S30-160
DirectionNeutral
Weight0.00841
VBMT 160408E-PC2 AT202
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.70-3.1
Feed (f)0.10-0.32
Cutting speed P50-200
Cutting speed K50-200
DirectionNeutral
Weight0.004
VBMT 160408E-PC2 AT210A
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.70-3.1
Feed (f)0.10-0.32
Cutting speed P50-180
DirectionNeutral
Weight0.0041
VBMT 160408-F2K AT202
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.3-2.0
Feed (f)0.13-0.30
Cutting speed P50-200
Cutting speed K50-200
DirectionNeutral
Weight0.004
VBMT 160408-F2K AT210A
Nose radius (r)0.8
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)0.50-2.0
Feed (f)0.10-0.25
Cutting speed P50-180
DirectionNeutral
Weight0.0041
No matching SKUs.
Turning guides
Supplied by Beijing Henglang Precision Tools Co., Ltd.