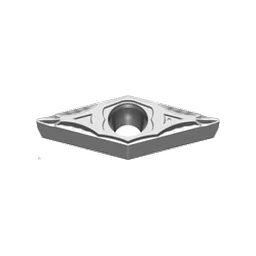
Achteck VBMT
Achteck VBMT 160412 Turning Inserts
BrandAchteckISO ModelVBMT160412Available MaterialsPKMSAvailable Options27
Available Applications
FinishingRoughingMedium
Specification
- ISO Code
- VBMT160412
- Insert Size
- 160412
- Shape
- V
- Radius
- 1.2 mm
- Thickness
- 4.76 mm
- D / IC
- 9.52 mm
- Hole Diameter
- 4.4 mm
- Available Materials
- PKMS
- Available Applications
- Finishing, Roughing, Medium
Product Overview
Achteck VBMT160412 inserts are grouped by the shared ISO parent model. Grade, chipbreaker, material suitability and technical parameters remain attached to each exact SKU.
Filter the table below and add the exact model you need to the RFQ basket.
Achteck VBMT160412
27 Available Options
| Full Model | Material | Application | Grade | Chipbreaker | Product No. | Quantity | Action |
|---|---|---|---|---|---|---|---|
VBMT 160412E-BS AC052P | P | Finishing | AC052P | BS | 80060687 | ||
VBMT 160412E-BS AC152P | P | Finishing | AC152P | BS | 80060701 | ||
VBMT 160412E-BS AC252P | P | Finishing | AC252P | BS | 80060715 | ||
VBMT 160412E-BS AT202 | PK | Finishing | AT202 | BS | 80048513 | ||
VBMT 160412E-BS AT210A | P | Finishing | AT210A | BS | 80048456 | ||
VBMT 160412E-KC2 AC052P | P | Roughing | AC052P | KC2 | 80051401 | ||
VBMT 160412E-KC2 AC100M | MS | Roughing | AC100M | KC2 | 80044298 | ||
VBMT 160412E-KC2 AC102K | K | Roughing | AC102K | KC2 | 80043458 | ||
VBMT 160412E-KC2 AC152P | P | Roughing | AC152P | KC2 | 80052449 | ||
VBMT 160412E-KC2 AC200M | MS | Roughing | AC200M | KC2 | 80044117 | ||
VBMT 160412E-KC2 AC202K | K | Roughing | AC202K | KC2 | 80043304 | ||
VBMT 160412E-KC2 AC252P | P | Roughing | AC252P | KC2 | 80052803 | ||
VBMT 160412E-KC2 AC350P | P | Roughing | AC350P | KC2 | 00034861 | ||
VBMT 160412E-KC2 AP200M | M | Roughing | AP200M | KC2 | 80040478 | ||
VBMT 160412E-KC2 AP200U | MS | Roughing | AP200U | KC2 | 80048968 | ||
VBMT 160412E-KC2 AT202 | PK | Roughing | AT202 | KC2 | 80028639 | ||
VBMT 160412E-KC2 AT210A | P | Roughing | AT210A | KC2 | 80059771 | ||
VBMT 160412E-PC2 AC052P | P | Medium | AC052P | PC2 | 80051393 | ||
VBMT 160412E-PC2 AC100M | MS | Medium | AC100M | PC2 | 80044267 | ||
VBMT 160412E-PC2 AC152P | P | Medium | AC152P | PC2 | 80052441 | ||
VBMT 160412E-PC2 AC200M | MS | Medium | AC200M | PC2 | 80044086 | ||
VBMT 160412E-PC2 AC252P | P | Medium | AC252P | PC2 | 80052795 | ||
VBMT 160412E-PC2 AP010S | MS | Medium | AP010S | PC2 | 80134767 | ||
VBMT 160412E-PC2 AP100S | MS | Medium | AP100S | PC2 | 00035080 | ||
VBMT 160412E-PC2 AP200M | M | Medium | AP200M | PC2 | 80040452 | ||
VBMT 160412E-PC2 AP200U | MS | Medium | AP200U | PC2 | 80048937 | ||
VBMT 160412E-PC2 AP301M | MS | Medium | AP301M | PC2 | 00037624 |
Cutting data and geometry (27 SKUs)
VBMT 160412E-BS AC052P
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-1.50
Feed (f)0.06-0.22
Cutting speed P105-620
DirectionNeutral
Weight0.0082
VBMT 160412E-BS AC152P
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-1.50
Feed (f)0.06-0.22
Cutting speed P95-570
DirectionNeutral
Weight0.0082
VBMT 160412E-BS AC252P
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-1.50
Feed (f)0.06-0.22
Cutting speed P75-510
DirectionNeutral
Weight0.008
VBMT 160412E-BS AT202
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-1.50
Feed (f)0.06-0.22
Cutting speed P50-200
Cutting speed K50-200
DirectionNeutral
Weight0.004
VBMT 160412E-BS AT210A
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-1.50
Feed (f)0.06-0.22
Cutting speed P50-180
DirectionNeutral
Weight0.0041
VBMT 160412E-KC2 AC052P
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-3.3
Feed (f)0.18-0.54
Cutting speed P105-620
DirectionNeutral
Weight0.008
VBMT 160412E-KC2 AC100M
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-3.3
Feed (f)0.18-0.54
Cutting speed M130-250
Cutting speed S30-80
DirectionNeutral
Weight0.008
VBMT 160412E-KC2 AC102K
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-3.3
Feed (f)0.18-0.54
Cutting speed K125-490
DirectionNeutral
Weight0.0085
VBMT 160412E-KC2 AC152P
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-3.3
Feed (f)0.18-0.54
Cutting speed P95-570
DirectionNeutral
Weight0.0079
VBMT 160412E-KC2 AC200M
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-3.3
Feed (f)0.18-0.54
Cutting speed M100-200
Cutting speed S20-70
DirectionNeutral
Weight0.0083
VBMT 160412E-KC2 AC202K
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-3.3
Feed (f)0.18-0.54
Cutting speed K95-400
DirectionNeutral
Weight0.0085
VBMT 160412E-KC2 AC252P
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-3.3
Feed (f)0.18-0.54
Cutting speed P75-510
DirectionNeutral
Weight0.0078
VBMT 160412E-KC2 AC350P
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.2-3.32
Feed (f)0.18-0.54
Cutting speed P45-250
DirectionNeutral
Weight0.00777
VBMT 160412E-KC2 AP200M
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.2-3.32
Feed (f)0.18-0.54
DirectionNeutral
Weight0.0082
VBMT 160412E-KC2 AP200U
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-3.3
Feed (f)0.18-0.54
Cutting speed M70-200
Cutting speed S30-90
DirectionNeutral
Weight0.0082
VBMT 160412E-KC2 AT202
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-3.3
Feed (f)0.18-0.54
Cutting speed P50-200
Cutting speed K50-200
DirectionNeutral
Weight0.0038
VBMT 160412E-KC2 AT210A
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.20-3.3
Feed (f)0.18-0.54
Cutting speed P50-180
DirectionNeutral
Weight0.0039
VBMT 160412E-PC2 AC052P
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.05-3.1
Feed (f)0.16-0.48
Cutting speed P105-620
DirectionNeutral
Weight0.008
VBMT 160412E-PC2 AC100M
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.05-3.1
Feed (f)0.16-0.48
Cutting speed M130-250
Cutting speed S30-80
DirectionNeutral
Weight0.0081
VBMT 160412E-PC2 AC152P
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.05-3.1
Feed (f)0.16-0.48
Cutting speed P95-570
DirectionNeutral
Weight0.0079
VBMT 160412E-PC2 AC200M
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.05-3.1
Feed (f)0.16-0.48
Cutting speed M100-200
Cutting speed S20-70
DirectionNeutral
Weight0.0083
VBMT 160412E-PC2 AC252P
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.05-3.1
Feed (f)0.16-0.48
Cutting speed P75-510
DirectionNeutral
Weight0.0078
VBMT 160412E-PC2 AP010S
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.05-3.1
Feed (f)0.16-0.48
Cutting speed M100-250
Cutting speed S30-120
DirectionNeutral
Weight0.0083
VBMT 160412E-PC2 AP100S
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.05-3.11
Feed (f)0.16-0.48
Cutting speed M85-240
Cutting speed S30-200
DirectionNeutral
Weight0.00848
VBMT 160412E-PC2 AP200M
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.05-3.11
Feed (f)0.16-0.48
DirectionNeutral
Weight0.0082
VBMT 160412E-PC2 AP200U
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.05-3.1
Feed (f)0.16-0.48
Cutting speed M70-200
Cutting speed S30-90
DirectionNeutral
Weight0.0082
VBMT 160412E-PC2 AP301M
Nose radius (r)1.2
Inscribed circle9.52
Thickness (s)4.76
Hole diameter (d1)4.4
Depth of cut (ap)1.05-3.11
Feed (f)0.16-0.48
Cutting speed M70-200
Cutting speed S30-160
DirectionNeutral
Weight0.0082
No matching SKUs.
Turning guides
Supplied by Beijing Henglang Precision Tools Co., Ltd.