INDEXABLE INSERTS
SCMT Turning Inserts
Compare SCMT parent models by material and application before choosing a brand.
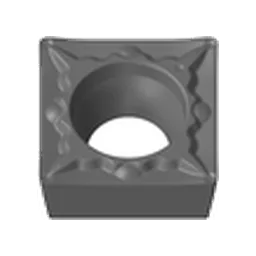
SCMT HADSTO, Achteck
SCMT 09T304
SCMT 09T304 indexable turning inserts. 41 available options.
SCMT HADSTO, Achteck
SCMT 09T308
SCMT 09T308 indexable turning inserts. 44 available options.
SCMT Achteck
SCMT 120404
SCMT 120404 indexable turning inserts. 31 available options.
SCMT Achteck
SCMT 120408
SCMT 120408 indexable turning inserts. 25 available options.
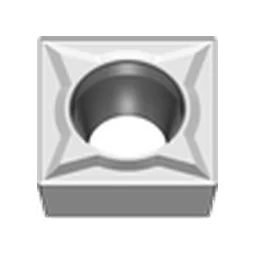
SCMT Achteck
SCMT 120412
SCMT 120412 indexable turning inserts. 18 available options.
No matching parent models.
This is our SCMT range: 6 sizes, 161 variants, Achteck, HADSTO. The geometry is a square 90° shape giving eight cutting edges and the strongest edge of any common insert. Applications published for the family cover Steel, Stainless steel, Cast iron, Non-ferrous, Heat-resistant alloys.
Sizes in this family
Every SCMT size we carry, with the measured geometry and how many variants are in stock. Open a size for the full cutting data and grade list.
| Size | IC (mm) | Thickness (mm) | Nose radius (mm) | Variants | Material groups |
|---|---|---|---|---|---|
| SCMT 09T308 | 9.53 | 3.97 | 0.8 | 44 | P, M, K, N, S |
| SCMT 09T304 | 9.53 | 3.97 | 0.4 | 41 | P, M, K, N, S |
| SCMT 120404 | 12.7 | 4.76 | 0.4 | 31 | P, M, K, S |
| SCMT 120408 | 12.7 | 4.76 | 0.8 | 25 | P, M, K, S |
| SCMT 120412 | 12.7 | 4.76 | 1.2 | 18 | P, M, K, S |
| SCMT 380932 | 38.1 | 9.53 | 2.4 | 2 | P |
Grades stocked in this family
AC350P, AP200U, AC052P, AC100M, AC152P, AC200M, AC252P, AP200M, AC102K, AC202K, AP100S, AT202, AT210A, AP301M, AC100K, HS6120, HS7125, HS7225 and others.
The family is published for Steel, Stainless steel, Cast iron, Non-ferrous, Heat-resistant alloys. Pick the grade from the group you are cutting — how to read grade names.
Chipbreaker geometries
KC2, PC2, PB2, PB1, M2T, PC4, PD9. The chipbreaker defines the feed window — chipbreaker selection guide.
Typical operations
- Medium
- Roughing
- Finishing
Which size do you need?
- Inscribed circle sets the maximum depth of cut. As a rule keep ap under about two thirds of the IC.
- Nose radius trades finish against strength. A larger radius gives better surface finish at the same feed and a stronger edge, but raises cutting force and cannot produce tight internal corners.
- Check the holder. The holder designation must carry the same shape letter and the same size digit as the insert.