INDEXABLE INSERTS
VCMT Turning Inserts
Compare VCMT parent models by material and application before choosing a brand.
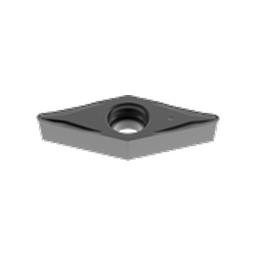
VCMT Achteck
VCMT 110302
VCMT 110302 indexable turning inserts. 1 available option.
VCMT Achteck
VCMT 110304
VCMT 110304 indexable turning inserts. 9 available options.
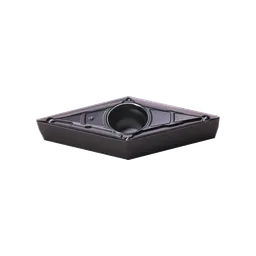
VCMT HADSTO
VCMT 110304-MV
VCMT 110304-MV indexable turning inserts. 5 available options.
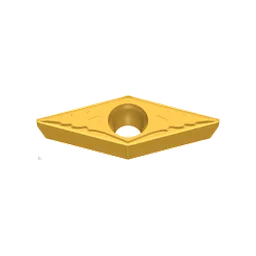
VCMT Achteck
VCMT 160402
VCMT 160402 indexable turning inserts. 1 available option.
VCMT Achteck
VCMT 160404
VCMT 160404 indexable turning inserts. 15 available options.
VCMT HADSTO
VCMT 160404-MV
VCMT 160404-MV indexable turning inserts. 5 available options.
VCMT Achteck
VCMT 160408
VCMT 160408 indexable turning inserts. 15 available options.
VCMT HADSTO
VCMT 160408-MV
VCMT 160408-MV indexable turning inserts. 5 available options.
No matching parent models.
VCMT is a 35° rhombic shape with four edges, for fine profiling, copying and sharp internal corners. There are 9 sizes in this family and 64 insert variants in stock, covering Steel, Stainless steel, Cast iron, Non-ferrous, Heat-resistant alloys.
Sizes in this family
Every VCMT size we carry, with the measured geometry and how many variants are in stock. Open a size for the full cutting data and grade list.
| Size | IC (mm) | Thickness (mm) | Nose radius (mm) | Variants | Material groups |
|---|---|---|---|---|---|
| VCMT 160404 | 9.53 | 4.76 | 0.4 | 15 | P, M, S |
| VCMT 160408 | 9.53 | 4.76 | 0.8 | 15 | P, M, S |
| VCMT 110304 | 6.35 | 3.18 | 0.4 | 9 | P, M, S |
| VCMT 110308 | 6.35 | 3.18 | 0.8 | 8 | P, M, S |
| VCMT 110304-MV | 6.35 | 3.18 | 0.4 | 5 | P, M, K, N |
| VCMT 160404-MV | 9.53 | 4.76 | 0.4 | 5 | P, M, K, N |
| VCMT 160408-MV | 9.53 | 4.76 | 0.8 | 5 | P, M, K, N |
| VCMT 110302 | 6.35 | 3.18 | 0.2 | 1 | P, M |
| VCMT 160402 | 9.53 | 4.76 | 0.2 | 1 | P, M |
Grades stocked in this family
AP200U, AC052P, AC100M, AC152P, AC200M, AC252P, AP200M, AP301M, HS6120, HS7125, HS7225, HS8115, HS8125.
The family is published for Steel, Stainless steel, Cast iron, Non-ferrous, Heat-resistant alloys. Pick the grade from the group you are cutting — how to read grade names.
Chipbreaker geometries
PB2, PC2, MV, PB1. The chipbreaker defines the feed window — chipbreaker selection guide.
Typical operations
- Medium
- Finishing
- Roughing
Which size do you need?
- Inscribed circle sets the maximum depth of cut. As a rule keep ap under about two thirds of the IC.
- Nose radius trades finish against strength. A larger radius gives better surface finish at the same feed and a stronger edge, but raises cutting force and cannot produce tight internal corners.
- Check the holder. The holder designation must carry the same shape letter and the same size digit as the insert.