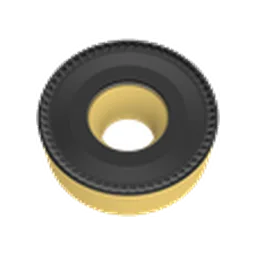
RCMT 2006 Turning Inserts
Compare suitable materials and applications, then choose a brand to view the exact SKUs.
- ISO Code
- RCMT2006
- Insert Size
- 2006
- Shape
- R
Find the Right Option
Select the workpiece material and application. Brand remains optional.
Brands
All available options for this parent model.
This page covers every RCMT 2006 insert we can supply — 1 variants across Achteck, published for Steel. The round geometry gives it many cutting edges and makes it suitable for the strongest edge available — roughing, hard skins, long reach.
The designation encodes the geometry: the first letter is the shape (R), the following letter the clearance angle, then the tolerance class, then size, thickness and nose radius. If you want to check any of it, our ISO insert code decoder breaks the full string down character by character.
Geometry and dimensions
| Insert family | RCMT |
|---|---|
| Category | Turning Inserts |
| Shape | round (R) |
| Usable cutting edges | many |
| Inscribed circle (IC) | 6.35 mm |
| Thickness (S) | 20 mm |
| Fixing hole diameter (D1) | 6.5 mm |
| Hand | Neutral |
| Variants in stock | 1 |
| Brands | Achteck |
Recommended cutting data
The figures below are the manufacturers' published ranges, aggregated across the 1 variants listed on this page. The typical column is the median, which is where most shops end up running. Treat the full range as the envelope, not a target — start around 60–70% of it and work up.
| Workpiece material | Cutting speed vc (m/min) | Typical vc | Feed fn (mm/rev) | Depth of cut ap (mm) | Variants with data |
|---|---|---|---|---|---|
| Steel (P) | 105 – 620 | 105 – 620 | 0.21–1.26 | 2–8 | 1 of 1 |
To turn a cutting speed into a spindle speed for your actual diameter, use the cutting parameters calculator: n = vc × 1000 / (π × D).
Carbide grades available
1 variants of RCMT 2006 are stocked in these grades: AC052P.
Across this range the grades specified most often are AC052P. Within one brand's range, a higher middle digit usually means a tougher grade — better on interrupted cuts, slightly less wear resistant. See carbide grades explained for how to read the names.
Chipbreaker geometries
Chipbreakers stocked for RCMT 2006: PD8.
The chipbreaker sets the usable feed window far more than the depth of cut does. A roughing geometry run at finishing feed will not break the chip; a finishing geometry pushed into a roughing cut will chip. Match it to the feed you will actually run — chipbreaker selection guide.
Typical applications
- Roughing
For more on cutting steel, see our material-specific guide.